Chemical Pumps - Chemical Processing Industry
Important information about the different industries we create pumps for.
Amarinth pumps enjoy global acclaim in the chemical process industry. Engineered to withstand aggressive and corrosive liquids, they stand as a testament to durability and reliability. Our pumps offer unmatched versatility, with the capability to supply them in any cast alloy, ensuring compatibility with a wide range of chemical processes, from harsh acids to volatile solvents.
Our API 610, API 685 (magnetic drive) & ISO 5199 pumps feature a variety of sealing solutions tailored to the level of protection required, including configurations utilising magnetic drives and pressurised double seals. With inherent high efficiency, our pumps contribute to substantial cost savings over their lifetime. By minimising energy consumption and maintenance needs, they enhance operational efficiency throughout processing plants, resulting in significant reductions in lifetime costs.
Trust Amarinth for reliable, high-performance pumping solutions designed to meet the rigorous demands of the chemical production industry, ensuring smooth and efficient operations while minimising downtime and these associated expenses.
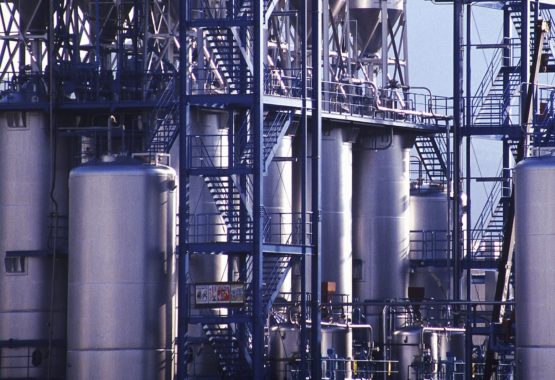
We strive to fully understand our customers’ requirements and ensure we deliver to your specifications and expectations within our quoted lead time. We currently deliver in excess of 95% of orders on-time, measured to the day.
We work closely with our customers to deliver exactly what is needed, on-time and on-budget, which we achieve through:
To find out more about us and how we operate and manage our contracts click here
We have successfully supplied products in the Chemical Pumps market to the following international projects in the table below:
We specialise in manufacturing pumps for these applications in the Chemical Pumps industry:
Acetic acids |
Biocide / rain |
Caustic transfer |
Chemical processing |
Dosing pumps |
Effluent treatment |
Foam |
Latex |
Liquid fertilizer |
Process Water |
Solvents |
Vinyl acetate monomer |
Wash Water |
Zinc slurry |
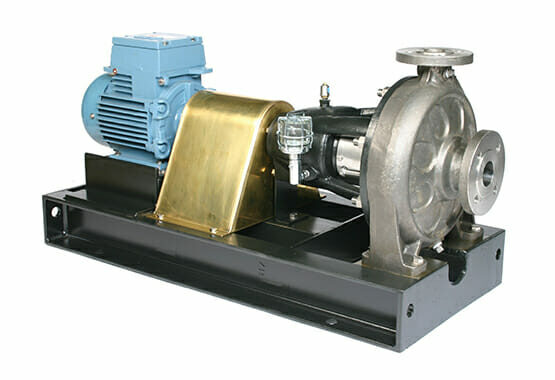
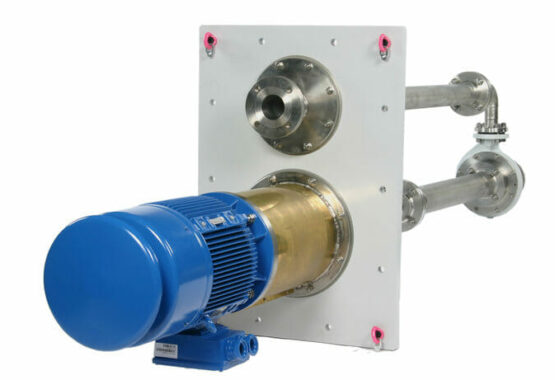
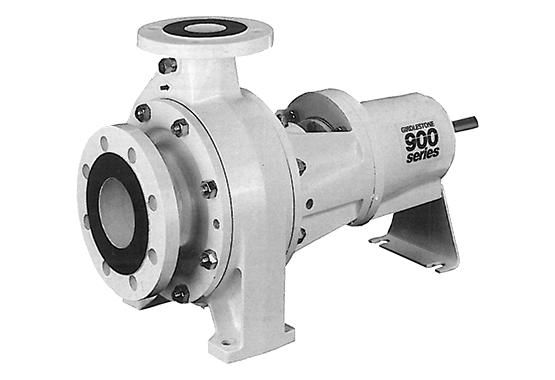
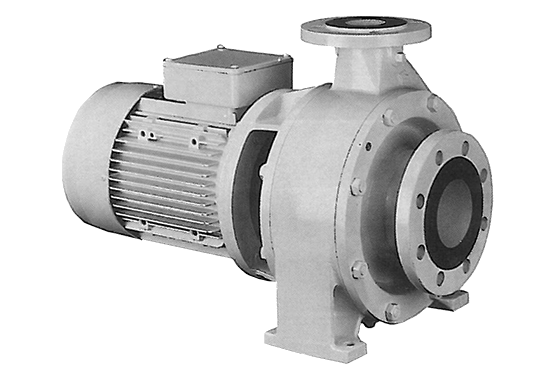
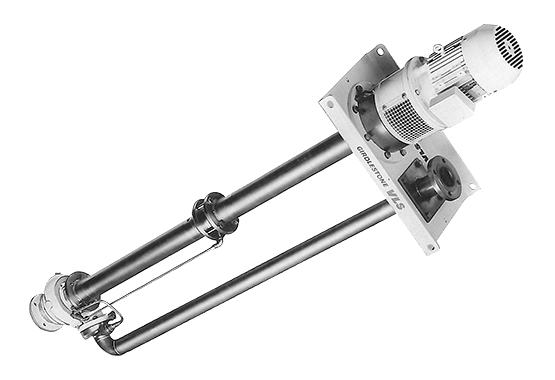
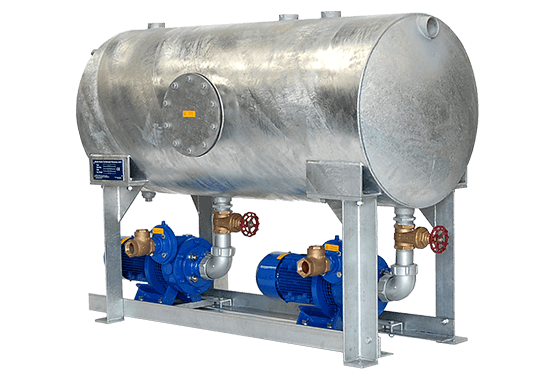
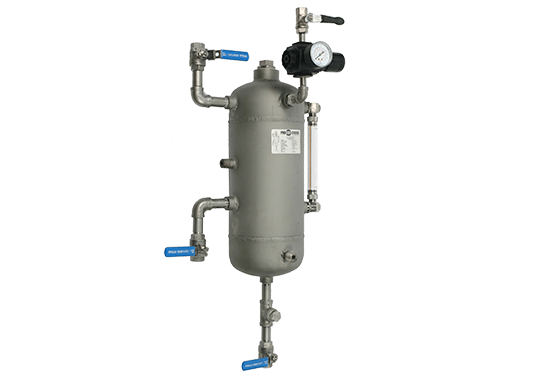
The following products are typically supplied by us into the Chemical Pumps Market.
We can customise our products to match you exact specification / requirement. Contact us to discuss your exact requirements
We have found 14 technical documents you may find of interest.
View our full library of documents relating to the Chemical Pumps Industry.
There are various health and safety regulations around the world that set the maximum continuous noise levels workers can be subject to, but all are broadly in agreement.
This form must be printed & completed before any pump is returned to our factory for repair or refurbishment. It should be faxed or e-mailed to Amarinth before the pump is sent. Pumps delivered to our factory without a decontamination certificate will be rejected and returned
Amarinth explains reverse engineering pitfalls and re-engineering benefits for Girdlestone 910 and 920 pumps
Amarinth explores the traditions of self-priming pumps and compares Amarinth products to traditional self-priming methods
Interpreting pump 'Tropicalisation' definition and the challenges faced by pump manufacturers to design equipment that can operate reliably in high temperature and humidity environments
Amarinth is independently verified by, accredited to or members of the following:





We work together to create innovative solutions which help our customers operate more efficiently and effectively.
Bentwaters Parks, Rendlesham, Woodbridge, Suffolk IP12 2TW. United Kingdom
tel: +44 (0)1394 462 120 fax: +44 (0)1394 462 130
e‑mail: sales@amarinth.com web: https://www.amarinth.com
Page printed from: https://www.amarinth.com/industries/chemical-processing/chemical-pumps